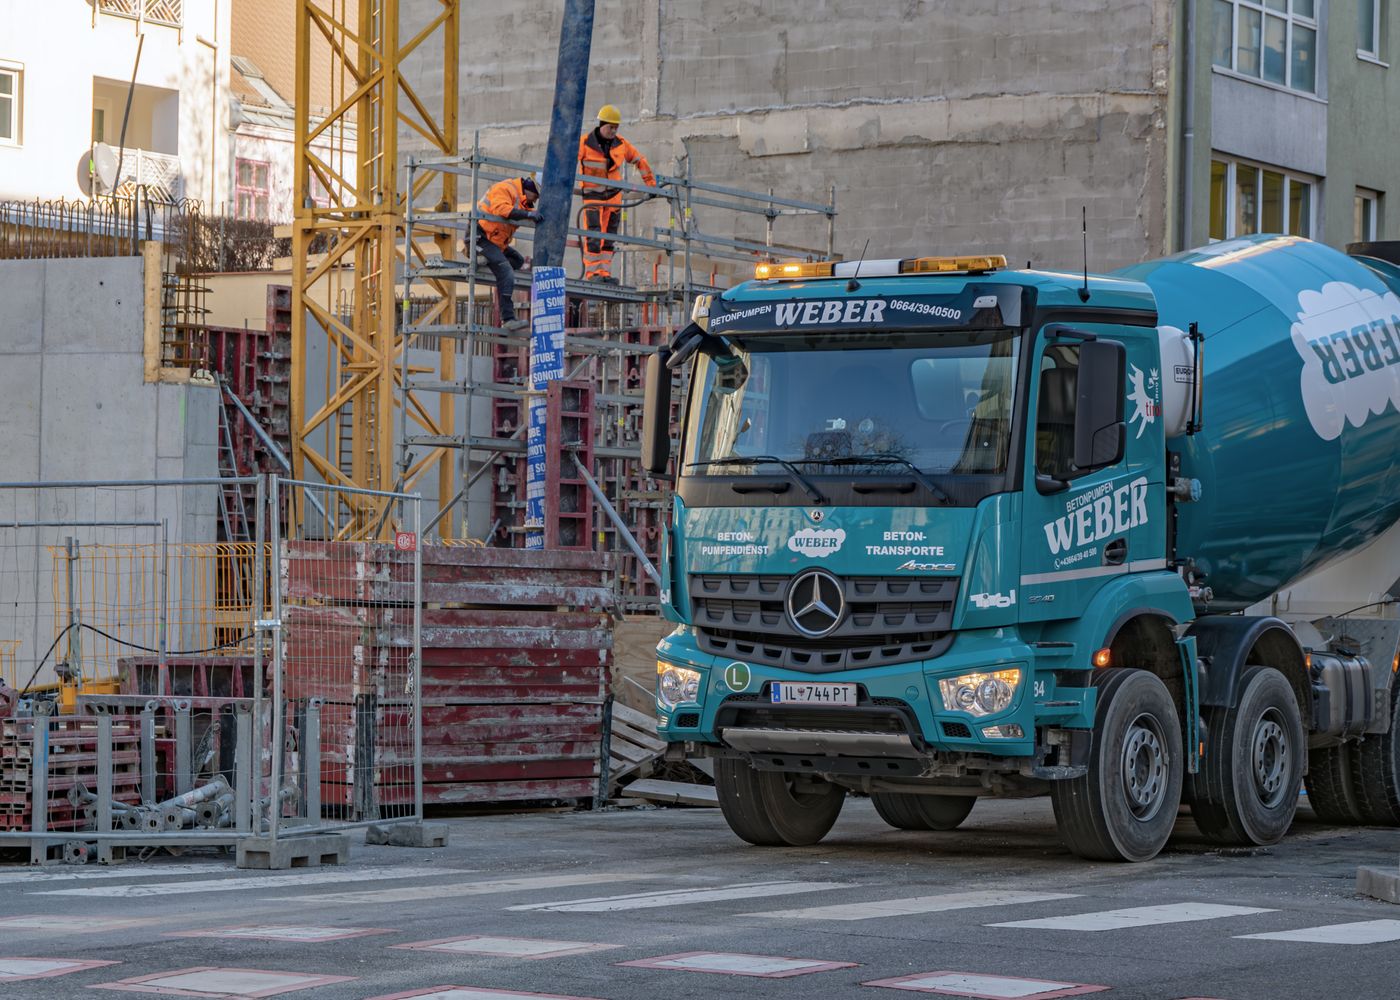
1. Document the chassis and mixer identities
Record chassis or VIN, model year, engine and transmission identifiers, mixer manufacturer, drum-capacity label, hydraulic pump and motor markings, and control arrangement. Compare these with the offered specification and service records. Ask who built or repaired the mixer body; chassis and mixer-equipment makers may differ.
2. Test drum and hydraulic functions
Under controlled conditions, observe drum rotation in both directions, speed control, hydraulic response, chutes, water system and fitted emergency stops or interlocks. Watch for leaks, vibration, uneven movement, unusual noise or visible damage. Record operating conditions; an empty run should not be described as a loaded-capacity test.
3. Inspect the road vehicle and define limits
Use a qualified commercial-vehicle inspector to review brakes, tires, steering, lights, frame, suspension and leaks. OSHA's checklist is a public example for basic road-safety items, not a mixer-equipment standard or substitute for local law. Separate checked, failed and untested items, and list repairs required before shipment or operation.
Separate an empty rotation check from a loaded test
Write the test result as an observation, not a broad performance claim. State whether the drum was empty, how long it ran, which controls were used and what the inspector could see. A smooth empty rotation can confirm basic movement, but it does not establish rated mixing capacity, loaded hydraulic performance or concrete quality.
Sources and further reading
This practical guide is an original summary based on the references below. Rules and technical requirements vary by market; verify current local requirements before purchase or export.